Custom Industrial Dehumidifiers Manufacturer - Delivered in 15 days.
What water quality is required for an ultrasonic humidifier?
Ultrasonic humidifiers need demineralised water. Most manufacturers specify reverse osmosis or deionised feed with total dissolved solids below 50 parts per million and conductivity in the range of 2 to 15 microsiemens per centimetre. Tap water above roughly 200 ppm leaves visible white dust, scales the transducers and shortens service life.
Why water quality decides whether the system survives
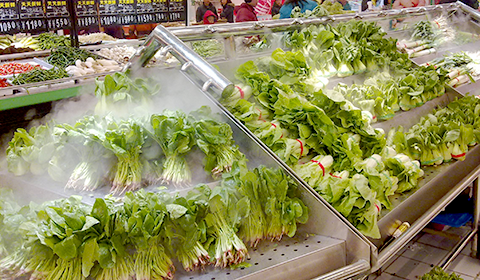
An ultrasonic humidifier does not boil water and it does not evaporate it from a wick — it atomises it. A piezoelectric disc vibrating at about 1.7–2.4 MHz shatters the water into 1–5 micron droplets, and those droplets contain everything that was dissolved in the water. The water evaporates in the air and the dissolved minerals stay airborne as fine white dust that settles on product, equipment and sensors.
That is the failure mode that gets ultrasonic systems removed from factories, and it is why reverse osmosis is part of the specification rather than an accessory. RO treatment removes roughly 95–99 percent of dissolved minerals. Published guidance is consistent across manufacturers: keep TDS below 50 ppm, or accept soft area supplies below about 100 ppm at the very most.
Manufacturer installation data is more precise than the rule of thumb. One major supplier specifies feed to the humidifier at 2–15 µS/cm conductivity, roughly 9 mg/L TDS, at 1–25 °C and 2–5.5 bar, with microbial count below 200 CFU/ml in and below 1,000 CFU/ml out. Their limits for the mains supply feeding the RO unit are far looser — up to 1,300 µS/cm and 800 mg/L depending on pH — which tells you where the treatment has to happen.
Two details catch people out. Drain piping must not be copper, because RO and DI water attack it. And extremely pure water can be a problem in the other direction: one instrument maker warns against distilled water below about 0.1 µS/cm because cavitation efficiency drops, so the target is demineralised, not maximally pure.
Representative project configuration
An assembly hall needed 45 ±5% RH through a dry winter for static control, with sensitive product on the line and no tolerance for mineral dust. Starting condition was 28% RH.
Units were ceiling-mounted on a grid with at least 2.5 m of clear evaporation distance to the nearest bench, and staged so only the number the load needs are running. The RO plant was costed into the project from the start — which is the point worth copying, because retrofitting water treatment after white dust appears costs more than specifying it up front.
Water specification and what each limit protects
| Parameter | Target at the humidifier | Mains limit into the RO stage | What it protects |
|---|---|---|---|
| Total dissolved solids | About 9 mg/L; <50 ppm acceptable | 375–800 mg/L by pH | White dust on product and sensors |
| Conductivity | 2–15 µS/cm | 600–1,300 µS/cm by pH | Scale formation on the transducer |
| Hardness | Effectively zero | 10–30 °dH by pH | Rotor and nozzle blockage |
| pH | 6.5–8.5 | 6.5–8.0 | Corrosion of internal components |
| Microbial count | <200 CFU/ml in, <1,000 CFU/ml out | 200 CFU/ml, no pathogens | Airborne contamination from the mist |
| Supply pressure | 2–5.5 bar, spikes limited to 8 bar | 2.0–5.0 bar | Stable output and seal life |
Two costs are routinely left out of ultrasonic comparisons and both are predictable: the water treatment plant, and transducer replacement. Transducer life is quoted at 12–24 months, or roughly 8,000–12,000 operating hours, and descale work with a citric acid solution at about 1:10 is a monthly task in hard water areas. East Dehumidifier treats the RO plant as part of the specification rather than an accessory, because white dust is the complaint that gets ultrasonic systems removed.
Related questions
Specifying water treatment?
Send your feed water analysis and required capacity. East Dehumidifier will size the units and specify the treatment that keeps white dust off your product.